AS9100 • ISO 9001 • ITAR REGISTERED
Fabtron Precision Fabrications
AEROSPACE • DEFENSE • PRECISION CONTRACT MANUFACTURING

Turnkey Precision Metal Fabrication for Aerospace & Defense Programs

Eliminate multi-week outsourced finishing delays. Fabtron Incorporated consolidates 4000W CNC laser cutting, TRUMPF multi-axis bending, large-envelope FANUC 12' × 35' robotic welding, and an in-house automated conveyor powder coating line under one roof in Plainville, CT.

Automated Raw ASRS 561,000 LBS 51 STOPA Pallets
CNC Laser Power 4000 WATT Nitrogen High-PSI
Robotic Weld Cell 12' × 35' Dual Turntables
Surface Finishing 100% IN-HOUSE Zero Freight Delay
Direct Plant Line: (860) 410-1801 • Principal Leadership: Garret J. Maino
✓
280-Ton Continuous Raw Material Inventory

Aluminum 6061-T6, 5052-H32, 304/316 stainless steel, and carbon steel stored on automated pallets ready for immediate blanking.

✓
Zero-Outsource Finishing Security

Automated overhead conveyor wash and electrostatic powder coating inside our secure facility—no transit damage or ITAR chain-of-custody breaks.

SUPPLY CHAIN RESILIENCE ARCHITECTURE

How Fabtron Collapses 10–14 Week Lead Times into 2–3 Weeks

Traditional sheet metal suppliers outsource forming, robotic welding, graining, or powder coating across multiple regional vendors. Fabtron unifies every production phase inside one 50-year established plant in Plainville, CT.

Fragmented Multi-Vendor Supply Chain 10–14 WEEKS
  1. 1
    Raw Material Lag (3–5 Days): No automated ASRS on floor; waiting for service center coil deliveries.
  2. 2
    Outsourced Press Brake or Weld Sub (2–3 Weeks): Parts packed onto flatbeds and trucked to third-party specialty weld shops.
  3. 3
    Commercial Coater Queue (3–4 Weeks): Parts sit in coater intake lots; batch runs delayed; frequent transit scratching and finger-pointing.
  4. 4
    ITAR Chain-of-Custody Failure Risk: Defense flight hardware moves through non-ITAR registered freight trucks and commercial finishers.
RESULT: High transit expense, 3 freight legs, repeated rework, 70–90 day delivery.
Fabtron Turnkey Single-Facility Model 2–3 WEEKS
  1. 1
    561,000 LB STOPA Raw Stock (Instant Intake): 51 automated pallets holding aerospace aluminum and stainless sheet ready immediately.
  2. 2
    TRUMPF 4000W Laser & 5130 Bending (Day 1–3): High-pressure nitrogen laser cutting directly shuttled to precision CNC press brakes.
  3. 3
    12'×35' Robotic Cell & AWS D17.1 GTAW (Day 4–7): Continuous automated arc welding and precision aerospace manual TIG in the same bay.
  4. 4
    In-House Overhead Conveyor Powder Coat (Day 8–10): Parts transfer directly via monorail from wash stage to powder application and cure. Zero road freight.
RESULT: 100% single-facility accountability, AS9100 quality gate, 14–21 day flight delivery.
CAPITAL MACHINERY ARCHITECTURE

Verified Plant Machinery • 80 Farmington Valley Drive

Every machine listed below is physically operating on our Plainville, CT shop floor. Explore technical specifications, working envelopes, and aerospace tolerances.

Complete Machine Registry →
Automated Sheet Handling 51 Pallets

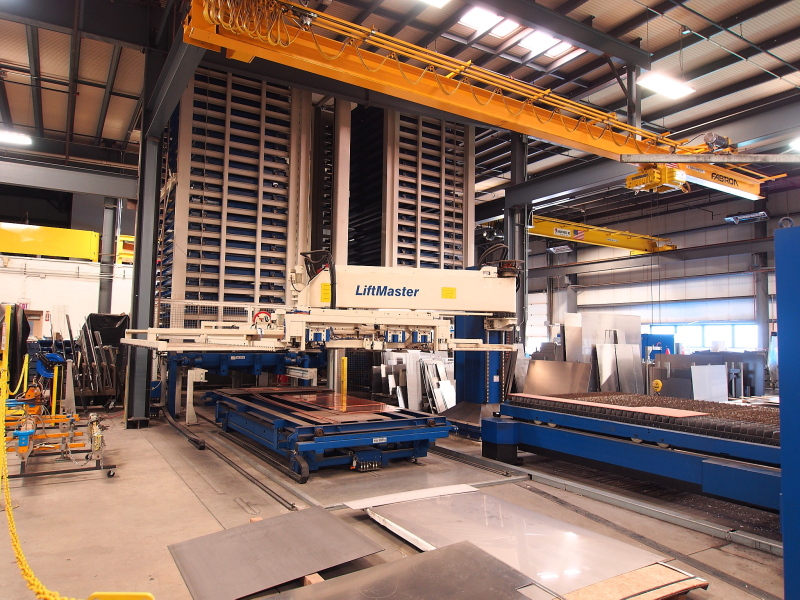
STOPA Vertical Storage + LiftMaster

51 automated storage cassettes with 11,000 lb capacity per pallet. Feeds TRUMPF LiftMaster automated vacuum loader directly into the CNC laser cutting bay.

• Live Inventory: 280 Tons Sheet Metal
• Sheet Size: Up to 60" × 120"
CNC Laser Cutting ±0.002" Accuracy

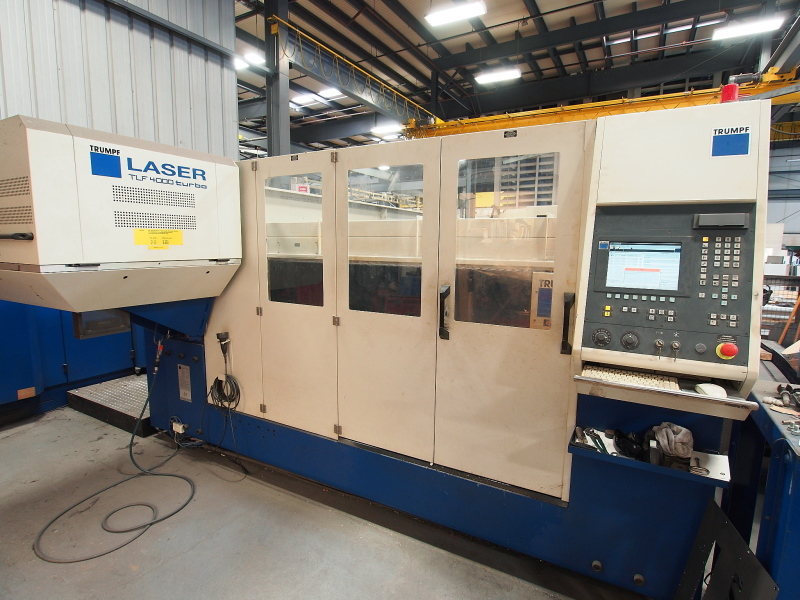
TRUMPF TLF 4000 Turbo Laser

Equipped with automated shuttle tables and high-pressure nitrogen assist cutting to deliver oxide-free, weld-ready edge quality on aerospace aluminum and stainless.

• Cutting Envelope: 60" × 120"
• High-Pressure N2 • Dual Shuttles
CNC Press Brake Forming 6-Axis Backgauge

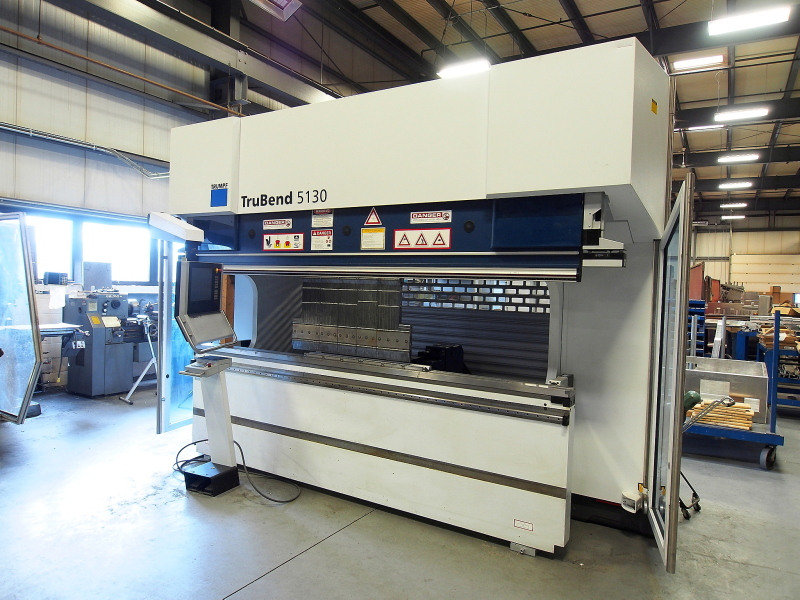
TRUMPF TruBend 5130

Multi-axis CNC backgauging with dynamic crowning compensation ensures razor-sharp angular accuracy (±0.25°) across extended lengths of aircraft chassis.

• Bed Length: 127 Inches (10.5 Feet)
• Dynamic Crowning • Precision Ground Dies
CNC Rotation Punching 360° Rotation

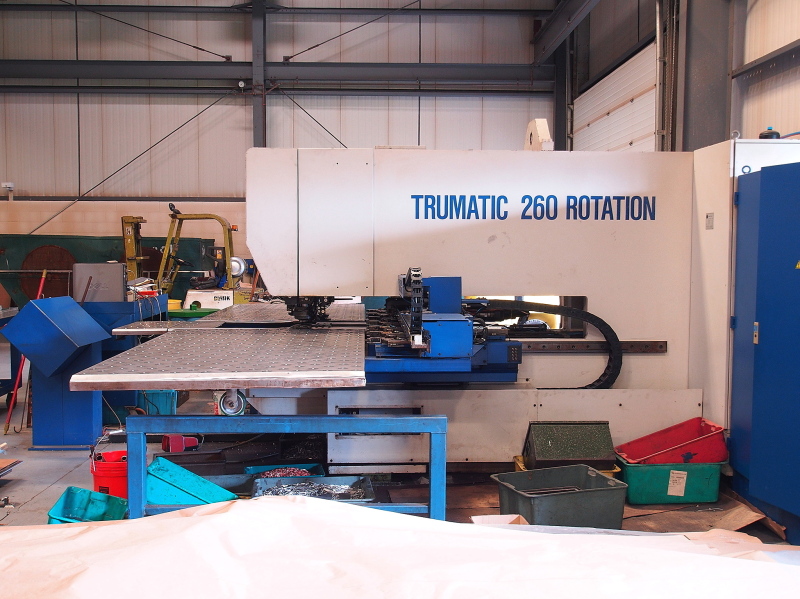
TRUMPF TruMatic 260 Punch

Full 360° tool rotation on all tool stations. Handles high-speed contour nibbling, louvers, card guides, countersinks, and automated M3–M8 thread forming.

• Sheet Size: 50" × 100" Without Reposition
• Multi-Tool Stations • Extrusions & Tapping
Surface Finishing #4 Architectural

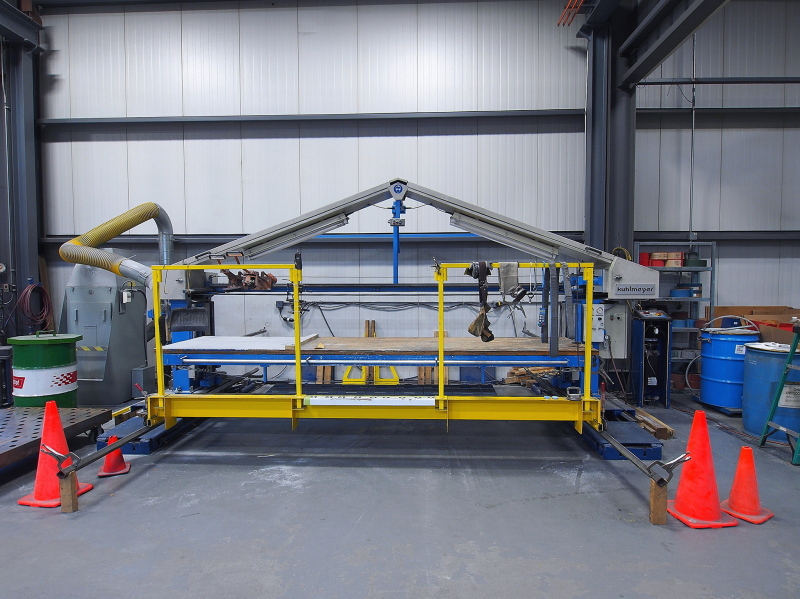
Kuhlmeyer Long-Belt Polisher

Large traveling gantry stroke sander producing flawless directional #4 satin finishes and blended welded seams on stainless turnstiles and aluminum flight chassis.

• Surface Roughness: Ra < 16 µin
• Seamless Corner Weld Graining
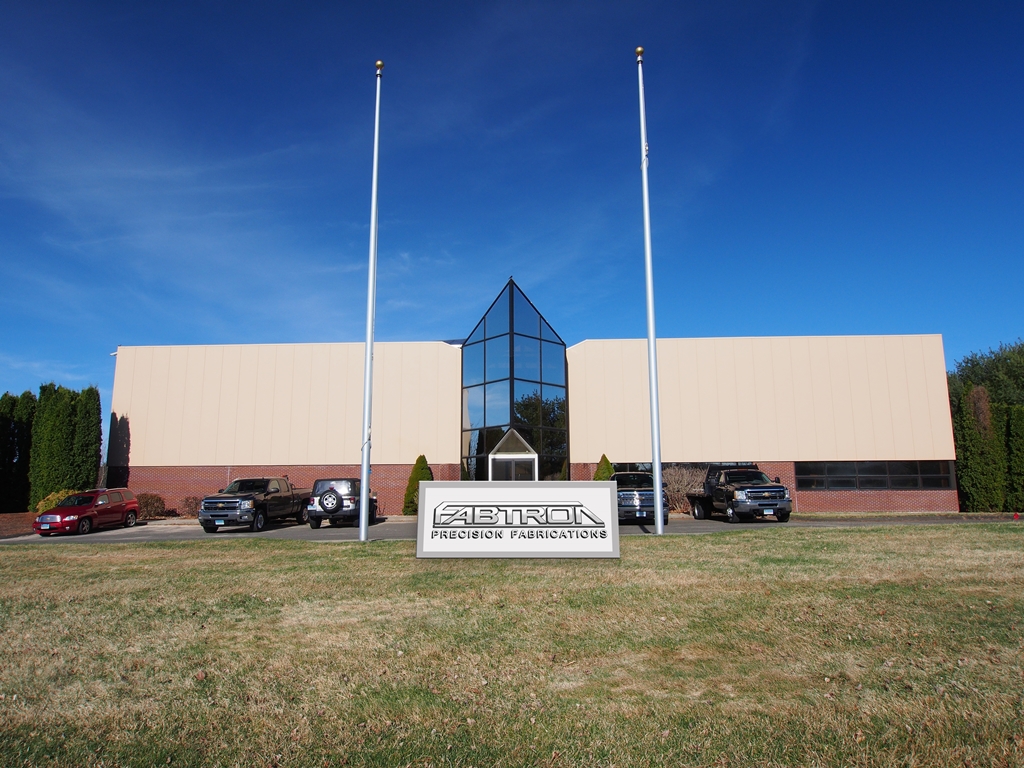
Connecticut Headquarters AS9100 / ITAR

80 Farmington Valley Drive

Centrally positioned in Connecticut's aerospace manufacturing corridor. Direct logistics to Pratt & Whitney, Sikorsky, Collins Aerospace, and General Dynamics Electric Boat.

• Owner & Principal: Garret J. Maino
• 10 Min from TRUMPF North America HQ
DEFENSE CAD • DFM REVIEW PORTAL

Fast-Track 3D CAD Intake & DFM Feedback

Directly upload 3D solid models and 2D flat drawings for rapid Design for Manufacturability (DFM) assessment. Our engineering staff in Plainville reviews bend radii, hole-to-bend clearances, and material grain direction before quotation.

Solid Models .STEP / .STP
Native CAD .SLDPRT / .IGES
Flat Patterns .DXF / .DWG
Digital Security & Compliance Protocol • 256-BIT TLS VAULT

ITAR Title 22 CFR Handling: Technical data submitted through Fabtron is protected in accordance with ITAR and EAR regulations. Data remains restricted to authorized US Persons.

Mutual NDA Protocols: Garret Maino and the executive engineering team execute standard non-disclosure agreements prior to reviewing classified aerospace or proprietary OEM drawings.

Direct Engineering Line: (860) 410-1801
DIRECT EXECUTIVE ENGINEERING CONSULTATION

Ready to Review Your Critical Metal Fabrication Project?

Speak directly with Garret Maino and our Plainville manufacturing engineers. Submit drawings for detailed DFM review and production quotations.