Precision contract manufacturing for high-throughput corporate headquarters, government facilities, and transit lobbies. Fabtron Incorporated fabricates luxury optical turnstile pedestals, motorized glass wing enclosures, and biometric access pillars in heavy-gauge 304 and 316 stainless steel with seamless weld graining.
High-end architectural turnstiles must combine jewelry-level exterior finishing with industrial-grade interior structural stiffness to absorb repeated passenger lateral force and motor torque.
Heavy 10-gauge structural baseplates and internal gusset towers laser cut on our TRUMPF 4000W system to anchor motor assemblies and eliminate pedestal deflection.
Precision CNC machined mounting plates for brushless DC servo drives, planetary gearboxes, magnetic brake clutches, and dual optical rotary encoders.
Flush-machined cutouts for HID Signo RFID readers, MorphoWave touchless biometric scanners, QR code windows, and infrared presence sensor arrays.
Precision CNC formed and clamped stainless barrier arm brackets holding 10mm to 12mm clear tempered or laminated architectural security glass wings.
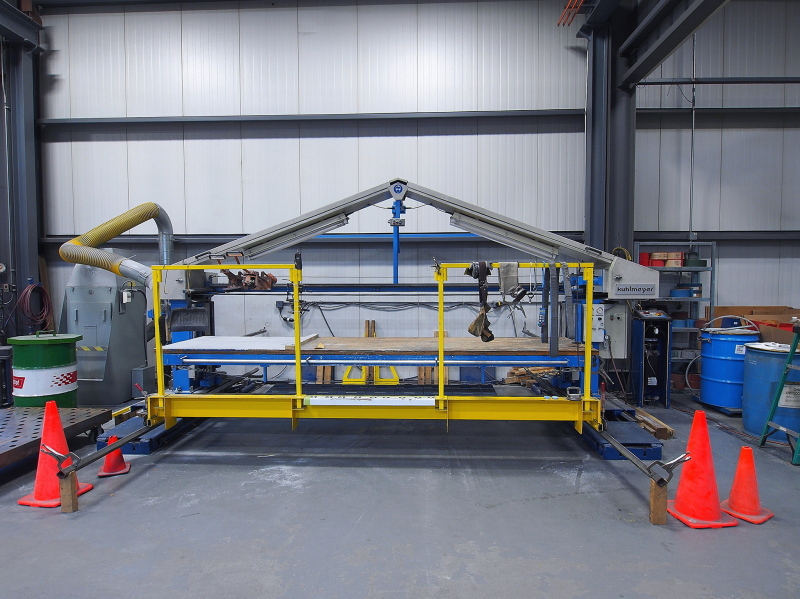
In visible corporate lobbies, hand-sanded grinder swirl marks and uneven weld seam blending ruin the look of high-end access gates. Fabtron eliminates this problem entirely with our verified Kuhlmeyer long-belt traveling stroke sander.
Comprehensive dimensional envelope and fabrication parameters for access control original equipment manufacturers.
| Engineering Parameter | Standard Specification | Manufacturing Tolerance | Fabtron Machine Equipment |
|---|---|---|---|
| Cabinet Length Envelopes | 48", 55", 60", and 72" custom lengths | ±0.010" | TRUMPF 4000W / TruBend 5130 |
| Pedestal Width & Height | 7.0" to 12.0" Width • 38.0" to 42.0" Height | ±0.005" | TRUMPF TruBend 5130 6-Axis |
| Laser Piercing & Cutouts | RFID, QR, Biometric & Infrared sensor cutouts | ±0.002" | High-Pressure Nitrogen Laser |
| Surface Roughness (Graining) | #4 Directional Satin Architectural Finish | Ra < 16 µin | Kuhlmeyer Long-Belt Sander |
| Fastener Installation | PEM® blind threaded standoffs & studs | Mil-Spec Push-Out | Haeger Automated Insertion |
How Fabtron controls 100% of quality from raw sheet retrieval to crating inside our 80 Farmington Valley Drive plant.
Raw 10, 12, or 14 gauge 304/316 stainless sheets automatically shuttled from our 561,000 LB inventory without distributor wait.
Clean, oxide-free laser cut edges with ±0.002" hole accuracy. Ready for immediate welding without edge grinding.
Dynamic crowning maintains precise 90.0° bend angles across 60-inch cabinet lengths with zero angle variance.
Certified TIG welding of cabinet corners with complete penetration and minimal heat input to prevent panel warping.
Traveling long-belt polisher blends all welded corners and produces flawless #4 directional architectural satin grain.
Full-surface adhesive protective film applied before foam-padded wooden crating to ensure zero transit scratching.
Design recommendations to optimize manufacturing speed, reduce tool setup, and achieve flawless lobby tolerances.
When designing return flanges on turnstile top lids, specify rectangular bend reliefs with a minimum depth of $T + R$ and width of $1.5T$ to prevent metal tearing at corner intersections.
Keep card reader cutout edges and sensor holes at least $2T + R$ away from bend tangents. This prevents hole elongation and distortion during press brake forming.
Ensure flat pattern nesting aligns with sheet grain orientation so that cabinet side panels and top lids have parallel, matching satin grain lines when assembled.
Answers to common technical questions from access control product managers, mechanical engineers, and security procurement teams.
We generally recommend 10-gauge (0.135") or 12-gauge (0.105") stainless steel for structural baseplates, motor bulkheads, and floor anchoring channels to eliminate deflection under pedestrian impact. For exterior aesthetic side panels and removable access lids, 14-gauge (0.075") or 12-gauge 304 stainless steel provides the ideal balance of rigidity, weight, and razor-sharp bend crispness.
We utilize our Kuhlmeyer long-belt traveling stroke sander using controlled abrasive grit sequences (typically 180 to 240 grit followed by non-woven conditioning belts) to calibrate surface roughness to Ra < 16 µin. We verify finish uniformity with optical surface roughness gages and provide physical finish coupon sign-offs prior to production runs.
Yes. Our TRUMPF 4000W CNC laser cuts mounting holes, countersinks, and flush display pockets to ±0.002" accuracy for HID Signo™, Allegion, IDEMIA MorphoWave™, facial recognition cameras, barcode scanners, and custom LED light pipes. Standoff studs and PEM nuts are pressed into place automatically.
Because we hold 561,000 lbs of raw sheet metal in our automated STOPA system and execute laser cutting, forming, welding, and graining 100% in-house in Plainville, CT, we typically deliver first-article prototypes in 2 to 3 weeks. Production batch quantities (20 to 200+ lane sets) are scheduled in predictable weekly releases.
Speak directly with Garret Maino and our Plainville manufacturing engineers. Submit STEP, IGES, or DXF files for rapid DFM analysis, tolerance optimization, and volume pricing.